01
Grooved piping systems
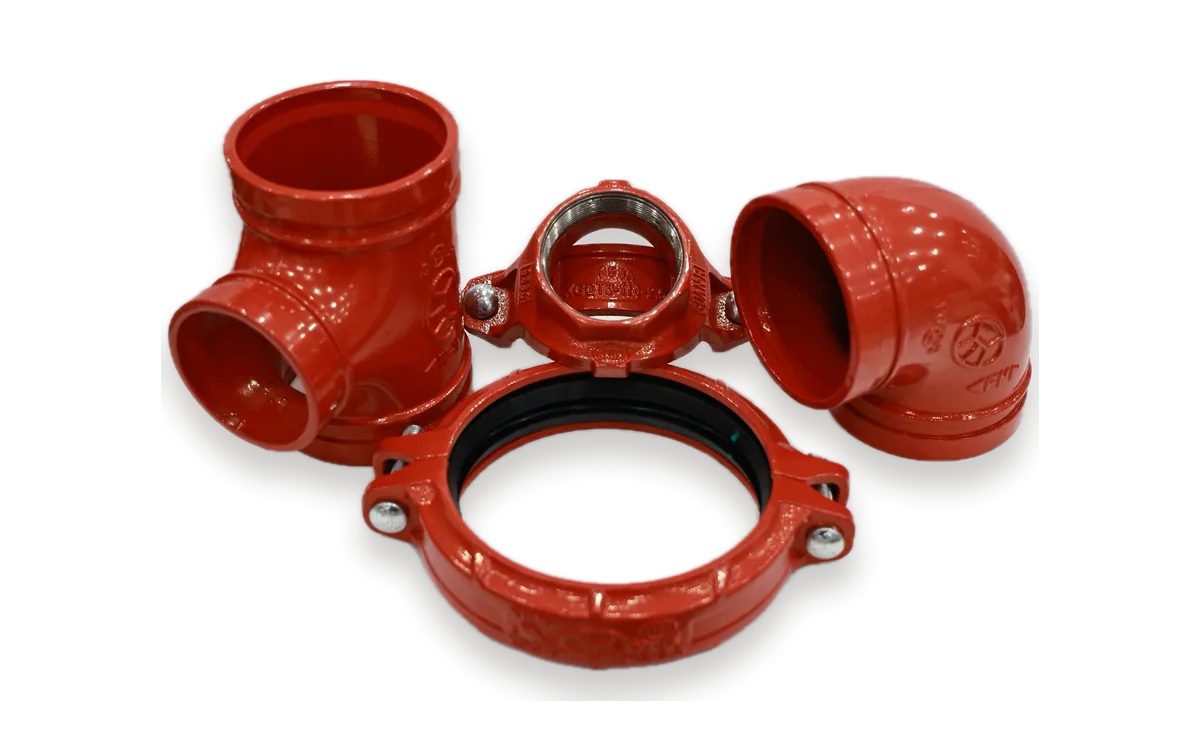
Rigid and flexible couplings, elbows, tees, crosses, mechanical tees, flange adaptors and caps for fire protection, water supply and HVAC piping.
UL Listed60–530 mmQT450-10
View range
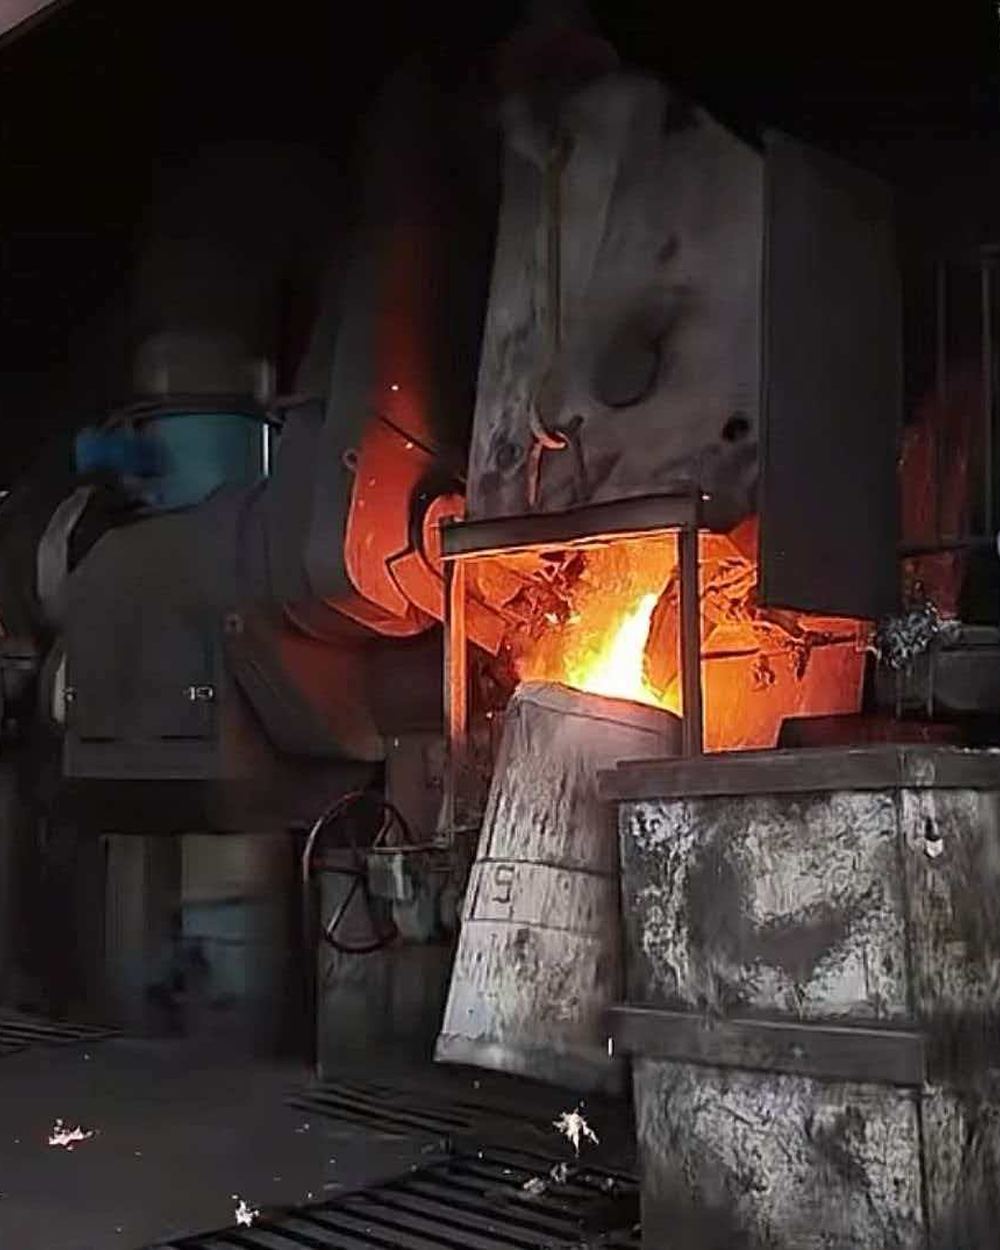
Shanxi, China — the heart of the country’s malleable iron industry. Two DISA moulding lines, six induction furnaces and an in-house pattern shop, under one roof with CNC machining, a metallurgical lab and 10,000 m² of automated warehousing.
One foundry, four product families — piping products sold under our own brand and into OEM programmes, and castings made to customer drawings.
Rigid and flexible couplings, elbows, tees, crosses, mechanical tees, flange adaptors and caps for fire protection, water supply and HVAC piping.
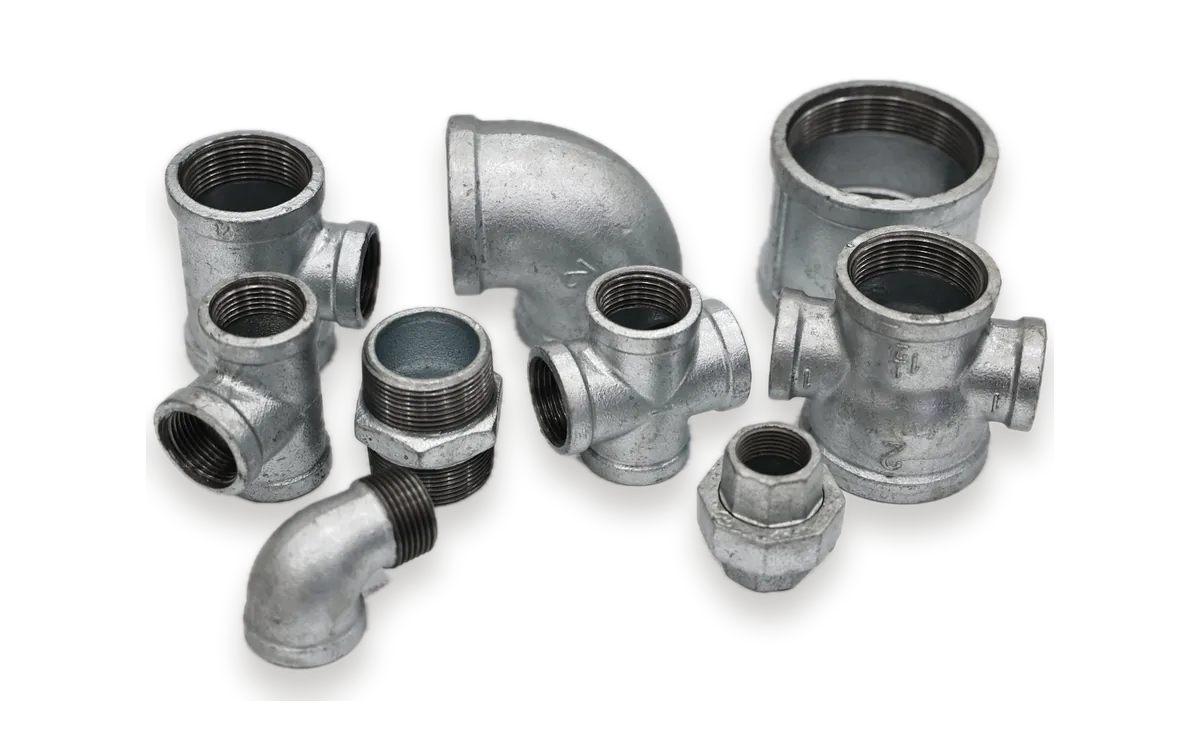
Threaded elbows, tees, crosses, sockets, unions, nipples, caps and bushings, black or hot-dip galvanised — FM Approved and UL Listed, plus PE/PP-lined for potable water.
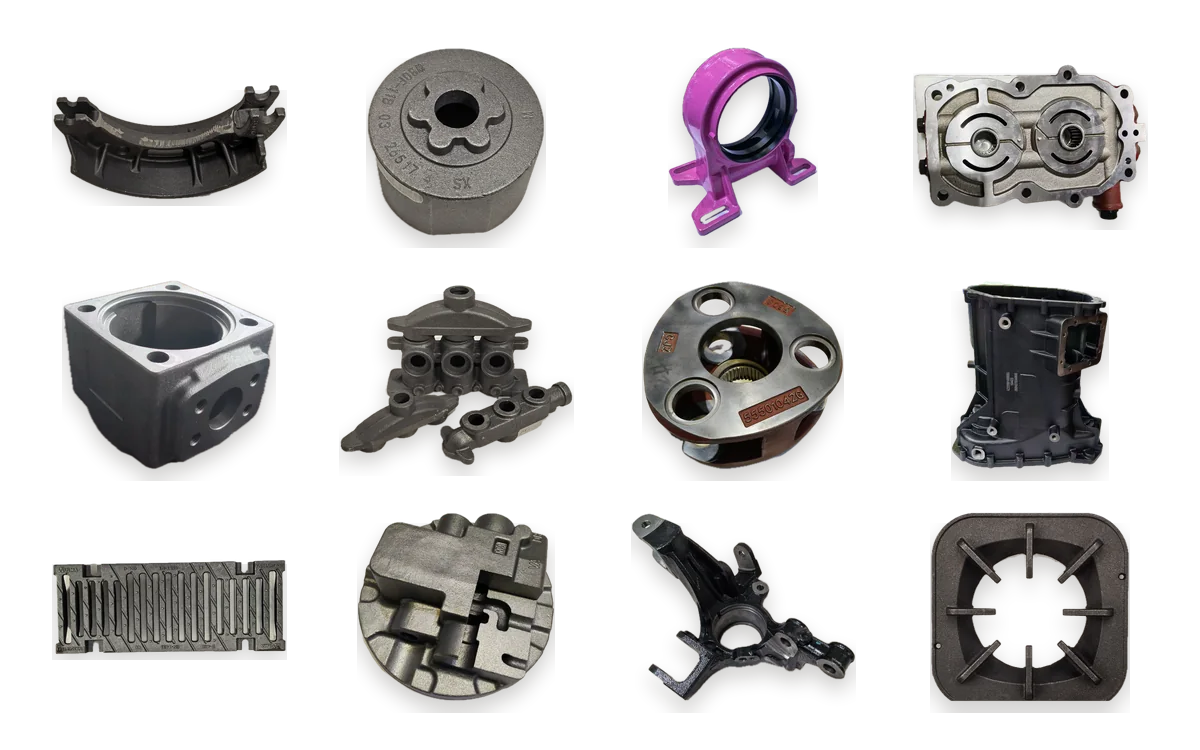
Ductile and grey iron components cast to your drawing: solar tracker parts, brake components, hydraulic housings, agricultural and construction machinery castings.
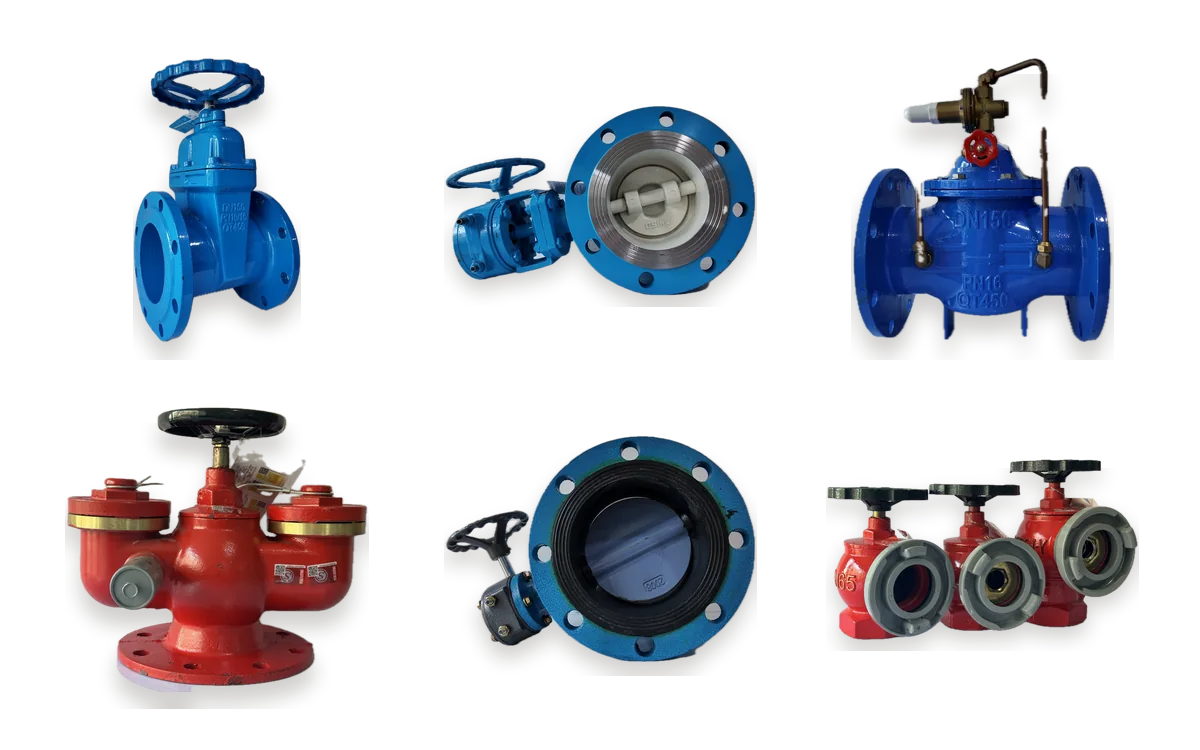
Resilient-seated gate valves, OS&Y gates, butterfly valves, swing check valves, Y-strainers and valve bodies, flanged to EN or ANSI drilling.
We are a single-site operation: melting, moulding, sand reclamation, machining, testing and warehousing all sit inside the same 80,000 m² campus. Nothing critical is outsourced, which is why our lead times hold and why a problem can be traced from a shipped carton back to the heat it was poured from.
Tianhe Casting has been pouring iron in Shanxi since 2005. Today the plant runs two imported Danish DISA vertical moulding lines, three domestic vertical lines and a resin-coated sand shell line with a 1,800 × 1,100 × 1,100 mm flask — the combination that lets us run both high-volume pipe fittings and heavier, low-volume OEM castings.
More about the plant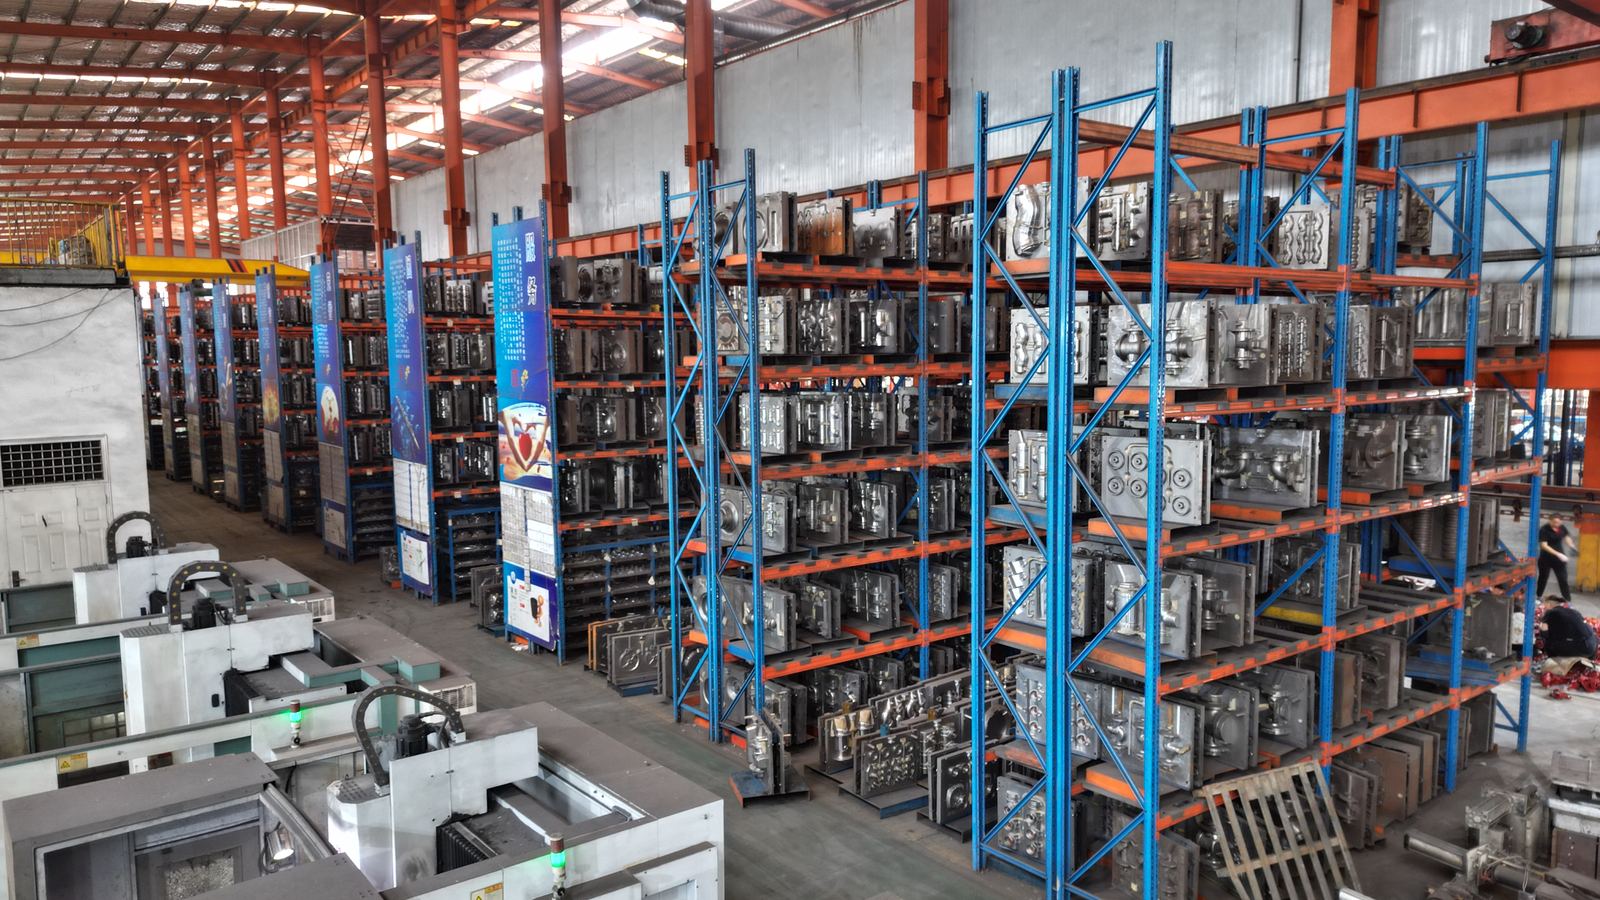
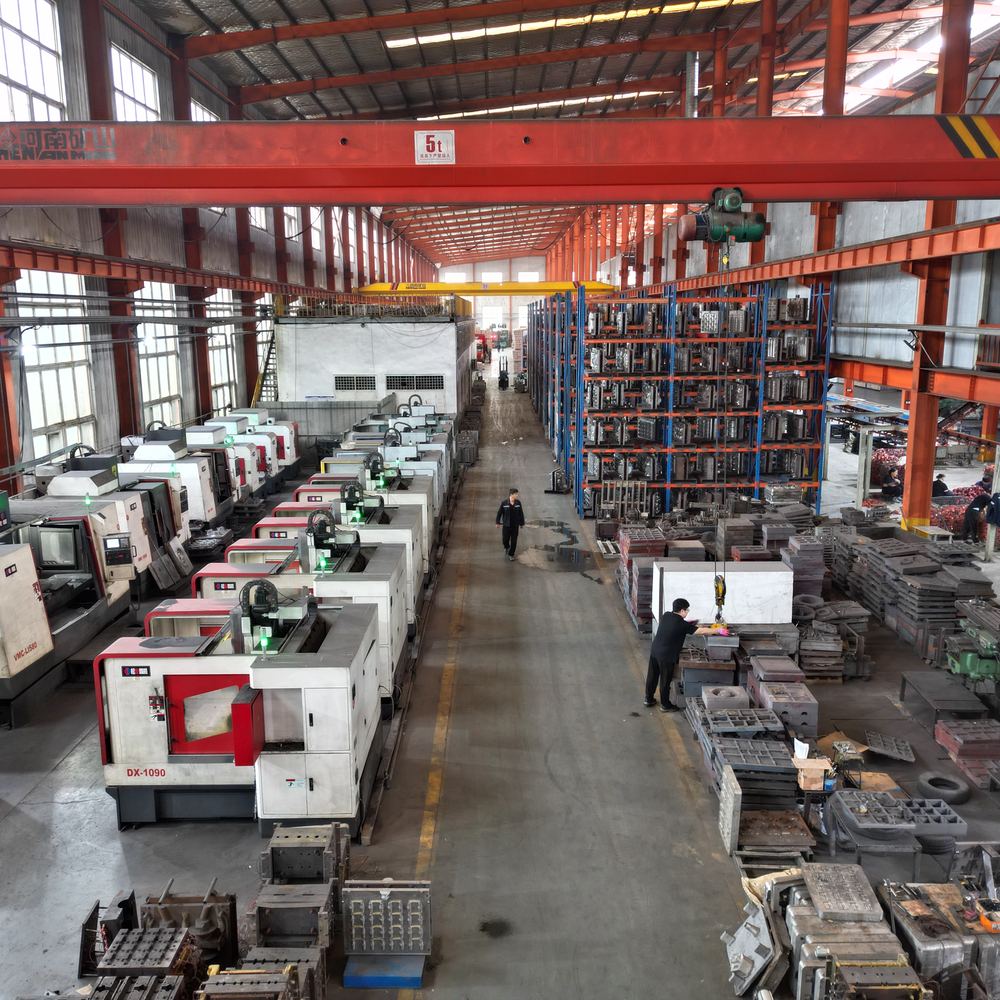
Eighty thousand tonnes a year, split between high-volume fittings and short-run OEM castings — with tooling made in-house so a new part does not wait months for a pattern.
Volume moulding and short-run work share the same melting and lab, so a 500-piece trial gets the same chemistry control as a 50,000-piece repeat order.
| Process | Equipment | Notes |
|---|---|---|
| Vertical moulding | 2 × DISA (Denmark), 3 × domestic | High-volume fittings |
| Shell moulding | Resin-coated sand line | Flask 1800 × 1100 × 1100 mm |
| Melting | 6 × Inductotherm 3 t | Ductile & grey iron |
| Sand plant | 2 × Fondarc lines | On-line moisture / compactability |
| Machining | 12 × 1160 centres, 50 lathes | Fixtures made in-house |
OEM programmes are the core of what we do. Tooling, sampling and validation are handled by the same team that runs production, so nothing gets lost between departments.
Send a 2D drawing or 3D model. We come back with a manufacturability review, tolerance callouts and a tooling proposal, usually within two working days.
Patterns and core boxes are designed and cut in our own tooling shop, so trial dates do not queue behind outside suppliers.
First-article castings ship with a dimensional report, material certificate and metallographic results for your approval.
Casting trials on DISA or shell lines, machining fixtures proven, control plan and inspection criteria agreed.
Repeat orders run on dedicated lines with SPC on critical dimensions; every heat is spectro-tested before pouring.
Machining, coating or galvanising, then export packing with photos and inspection records before dispatch.
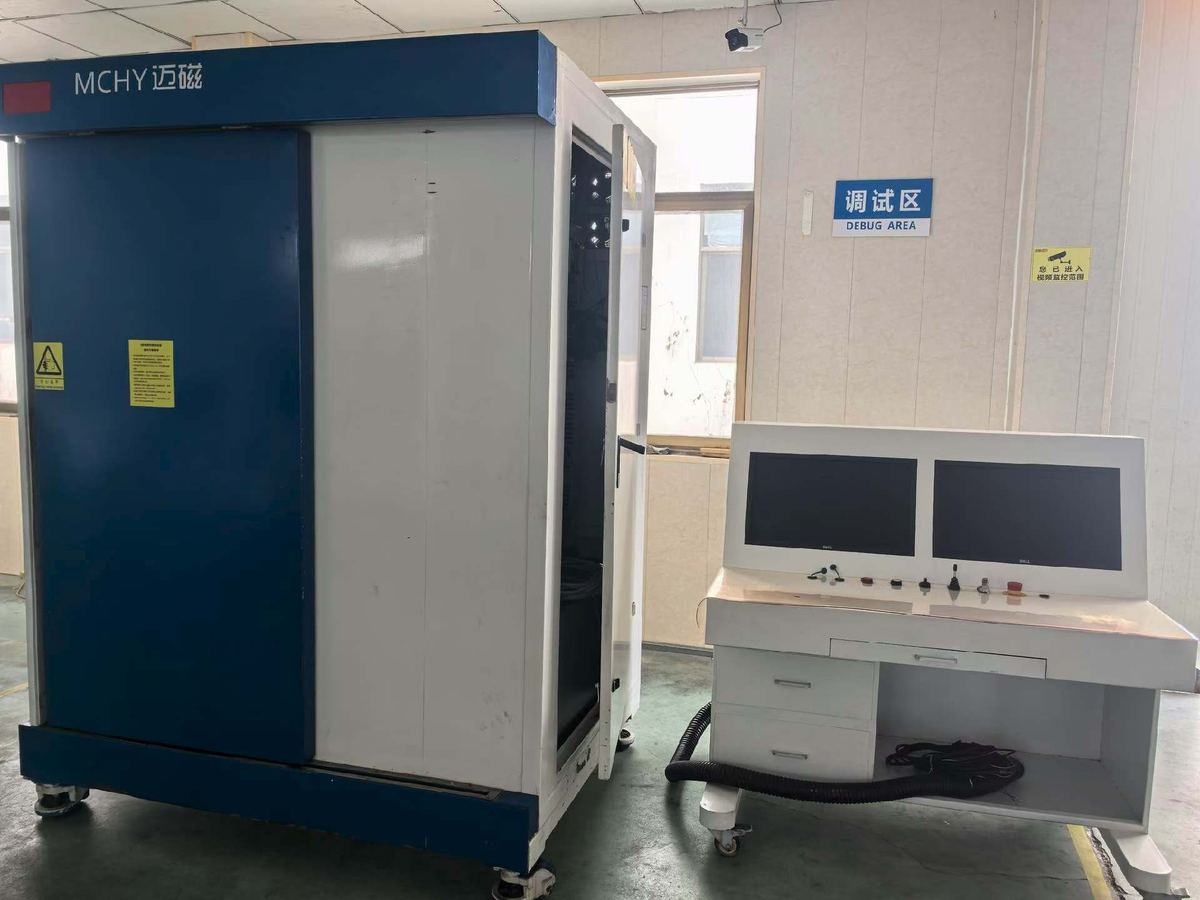
A Swiss ARL spectrometer reads 26 elements in about 30 seconds, so chemistry is corrected at the furnace rather than discovered after machining. Castings then go through metallography, hardness, tensile testing and, where the drawing calls for it, dimensional inspection on a CMM.
ARL optical emission spectrometer, 26 elements, 30 s; CS-9900 carbon–sulphur analyser.
Zeiss metallographic microscope, hardness tester, SANS electro-hydraulic servo tensile machine.
CMM, gauges and fixtures, plus flaw detection for porosity, shrinkage and cracks.
Full sand testing laboratory; both sand plants run on-line moisture and compactability control.
Piping products and castings ship across Europe, the Middle East, Southeast Asia, South America and Africa. Malleable iron fittings are held in stock by a partner in Brazil, who handles local technical support.
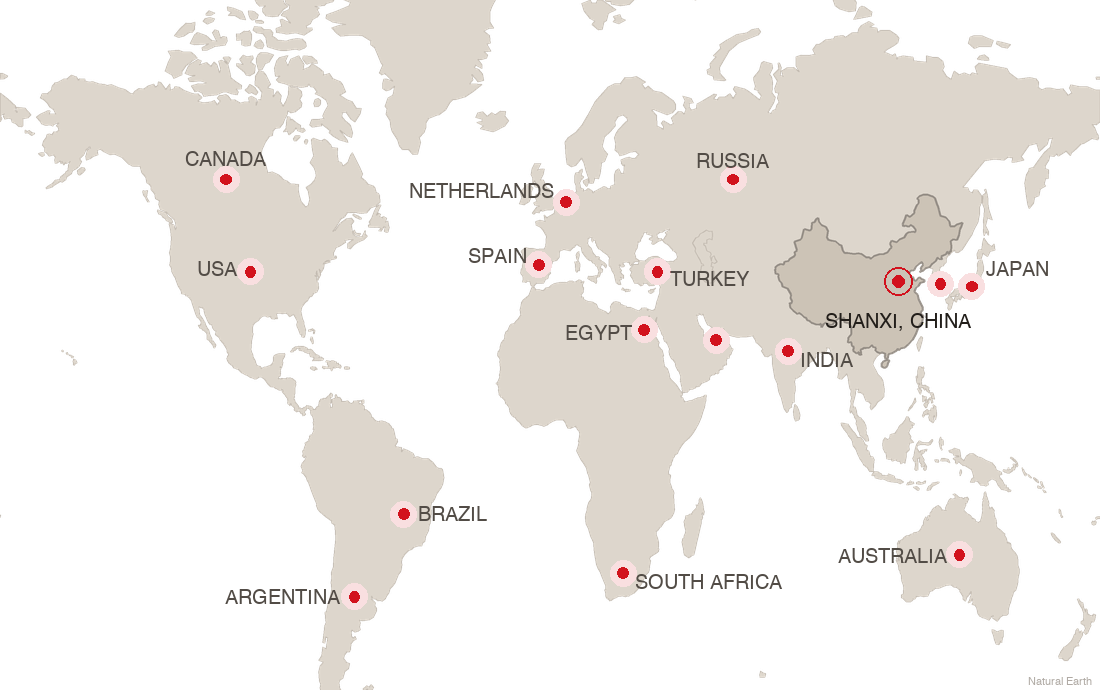
EXW, FOB and CIF terms; export packing to your forwarder’s requirements.
Material certificates, dimensional reports, inspection records and certificate of origin with every shipment.
Cast-in lettering, customer artwork on cartons and neutral packing for distributor brands.
Tell us the material, annual volume and destination port — we reply with a process review, tooling cost and piece price. If the part does not suit our lines, we will say so.